How Should Buyers Set AQL Sampling and Defect Criteria for Nonwoven Roll Inspection?
Before a bulk shipment of nonwoven rolls leaves the factory, overseas buyers need more than a simple visual inspection. A proper nonwoven pre-shipment inspection (PSI) should clearly define the sampling quantity, inspection items, defect classification, and acceptance criteria.
For buyers purchasing large quantities of nonwoven roll material, AQL sampling can provide a structured way to inspect a production lot without checking every roll. However, AQL should not be treated as a single number such as “AQL 2.5.” The inspection level, sampling plan, defect classification, and acceptance or rejection criteria should be agreed upon before the inspection.
Why Should Nonwoven Bulk Orders Not Be Inspected by Checking Only One Roll?
A bulk order of nonwoven material may contain dozens or hundreds of rolls. Checking only one roll can show the condition of that particular roll, but it cannot reliably represent the quality of the entire production lot.
During continuous nonwoven production, defects may appear at different stages or locations. For example, one roll may have a clean surface while another roll from the same production lot may contain holes, stains, foreign matter, edge damage, excessive joints, or variations in appearance.
For overseas buyers, the purpose of pre-shipment inspection is therefore not simply to find whether one roll has a defect. It is to determine whether the overall production lot meets the agreed purchasing requirements.
A properly defined sampling plan allows inspectors to select samples from the lot according to an agreed method instead of relying on a few manually selected rolls.
What Does AQL Actually Solve in Nonwoven Roll PSI?
AQL, or Acceptance Quality Limit, is used within an acceptance sampling system to determine how a production lot should be evaluated based on samples. The current ISO 2859-1:2026 standard provides AQL-indexed sampling schemes for lot-by-lot inspection by attributes.
For nonwoven roll inspection, AQL helps buyers establish a consistent relationship between the lot size, sample size, defect classification, and acceptance or rejection decision.
However, AQL itself is not a complete nonwoven quality specification.
For example, an inspection requirement that simply says “AQL 2.5” does not tell the inspector which defects should be treated as Major or Minor, which product specifications should be measured, how many joints are acceptable, or which packaging problems should cause rejection.
Therefore, buyers should define the complete inspection requirements rather than treating the AQL value as the entire quality standard.
What Should Be Defined First: Lot, Inspection Level and Sampling Plan?
Before a nonwoven pre-shipment inspection, the buyer and supplier should first agree on what constitutes the inspection lot and how samples will be selected.
The Lot should clearly identify the quantity being submitted for inspection. Depending on the purchasing agreement, this may be defined by one production batch, one shipment, one product specification, or another agreed unit.
The Inspection Level determines the relationship between lot size and sample size within the selected sampling system. The buyer should specify the applicable inspection level instead of leaving the inspector to make an informal decision.
The Sampling Plan then determines how many rolls or samples should be inspected and how the inspection result will be evaluated.
This is important because different lot sizes do not necessarily require the same number of samples. A structured AQL system provides a consistent basis for making that decision instead of simply inspecting a fixed percentage of rolls.
Which Defects Should Be Checked on Nonwoven Rolls?
A nonwoven roll defect checklist should cover both visual defects and measurable product requirements.
For visual inspection, buyers may define requirements for holes, stains, foreign matter, color variation, uneven surfaces, edge damage, wrinkles, contamination, and other visible defects that could affect the intended application.
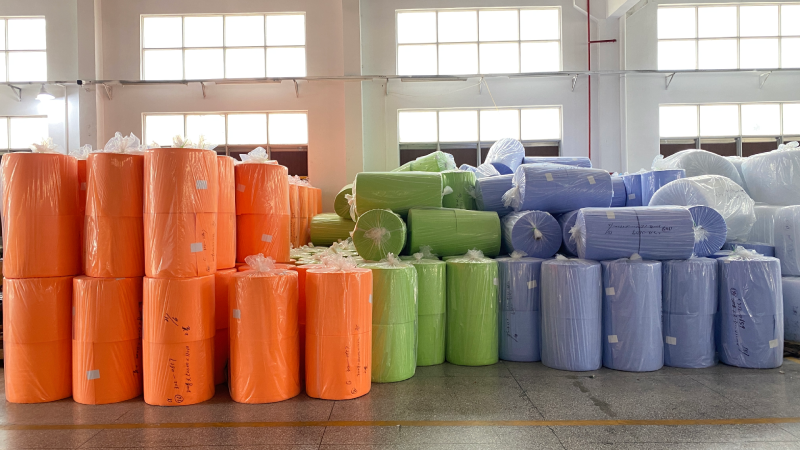
For roll specifications, inspectors may need to verify GSM, thickness, width, roll length, number of joints, and packaging condition according to the approved specification.
The inspection scope should be based on the actual product and its intended use. For example, a nonwoven material used for filtration may require different critical quality controls from a material used for floor protection, automotive interiors, acoustic applications, or industrial components.
The key point is that the inspection checklist should be agreed before shipment rather than created after defects are discovered.
How Should Major, Minor and Critical Defects Be Classified?
Defect classification helps the buyer and supplier distinguish between problems with different levels of impact.
A Critical Defect is a defect that may create a serious safety, regulatory, or essential-use risk. If a critical defect is possible for the specific application, the buyer should clearly define it and establish the corresponding acceptance requirement before production.
A Major Defect is a defect that can significantly affect the product's intended use, appearance, performance, or ability to meet the agreed specification. Examples may include serious surface damage, significant dimensional deviation, unacceptable material contamination, or other defects that make the roll unsuitable for its intended application.
A Minor Defect is a smaller deviation that does not normally prevent the product from being used as intended but may affect appearance or secondary requirements.
The exact classification should be agreed according to the product specification and application. Buyers should not assume that every nonwoven product should use the same defect classification.
How Should GSM, Width, Roll Length and Joint Count Be Included in Inspection Criteria?
Visual inspection alone is not enough for nonwoven roll quality inspection. Important physical specifications should also be included in the PSI requirements.
GSM should be checked against the agreed product specification and tolerance. A material that looks visually acceptable may still fail to meet the required basis weight.
Width should be measured at appropriate points to determine whether the finished roll remains within the agreed tolerance.
Roll length should be verified when the commercial specification is based on a defined length per roll. This is particularly important when buyers calculate the total material quantity based on roll length.
Joint count should also be clearly specified when the buyer requires continuous rolls with limited joints. The acceptable number of joints and the way joints should be identified should be agreed before production.
These requirements should be included in the inspection specification rather than left to the inspector's personal judgment.
Why Does Finding a Defect Not Automatically Mean the Entire Lot Must Be Rejected?
An important point for overseas buyers is that finding a defect is not automatically the same as rejecting the entire production lot.
Acceptance sampling is designed to make a lot-level decision based on a defined sampling procedure and acceptance criteria. ISO 2859-1:2026 provides AQL-indexed sampling schemes and acceptance/rejection rules for lot-by-lot inspection.
For this reason, the inspection result should be evaluated according to the agreed sampling plan and defect classification.
If the inspection identifies defects, the buyer and supplier should determine whether the result falls within the agreed acceptance criteria or exceeds the rejection criteria.
This distinction is important because an inspection report should not simply state “defects found” without explaining how those defects relate to the agreed acceptance standard.
How Should Overseas Buyers Put AQL Inspection Requirements into a Purchase Order?
For overseas procurement, the AQL requirement should be written into the purchasing documents before bulk production or shipment.
The specification should clearly state the inspection lot, applicable inspection level, sampling plan, AQL requirements, Critical/Major/Minor defect definitions, product measurements, visual inspection items, packaging requirements, and acceptance or rejection criteria.
For example, the buyer can specify that the PSI should evaluate the agreed nonwoven roll inspection requirements according to a defined AQL sampling system, while separately specifying tolerances for GSM, width, roll length, joint count, appearance, packaging, and labeling.
The buyer should also confirm whether inspection will be performed by the supplier's QC team, the buyer's representative, or an independent third-party inspection company.
Most importantly, these requirements should be confirmed before the inspection takes place. This helps prevent disputes caused by different interpretations of what constitutes an acceptable shipment.
How Can JHC Support Bulk Order Quality Control?
For overseas buyers sourcing needle punched nonwoven, nonwoven felt, floor protection materials, automotive nonwoven materials, acoustic felt, and other customized nonwoven products, stable bulk production and consistent quality are important parts of supplier evaluation.
HuiZhou JinHaoCheng Nonwovens Co., Ltd. has more than 20 years of nonwoven manufacturing experience and supports customized production for different product requirements. Its production and quality-control processes can be aligned with agreed product specifications and inspection requirements before bulk shipment.
For customized orders, buyers can confirm the required GSM, thickness, width, roll length, appearance, joint requirements, packaging, and other quality criteria during the order stage, creating a clearer basis for subsequent production inspection and shipment approval.
Conclusion
A practical nonwoven roll AQL inspection should not be reduced to choosing a number such as AQL 2.5. The buyer needs to define the inspection lot, inspection level, sampling plan, defect classification, product specifications, and acceptance or rejection criteria in advance.
For overseas buyers, this approach makes pre-shipment inspection more consistent and reduces disagreements between the buyer, supplier, and inspection company. More importantly, it connects the PSI process with the actual purchasing requirements rather than treating AQL as a standalone quality specification.